 EN
 RU
High-Mix Case Forming, Robotic Packing and Sealing Line for Sanitary Napkins
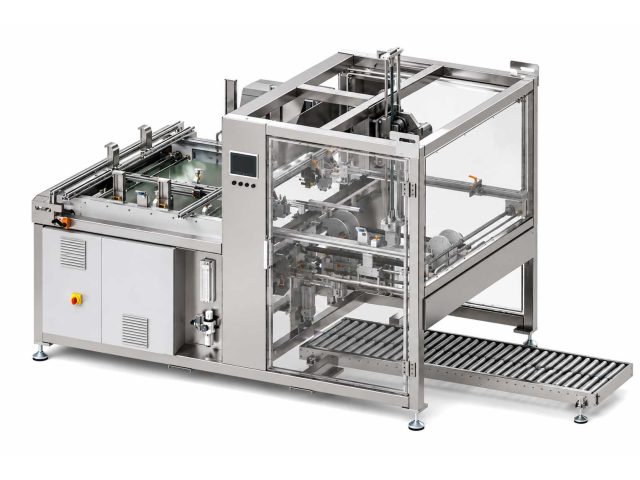
More than 30 SKUs on one case packing line with a 5-minute changeover — case forming, robotic vision packing and sealing in a single cell.
Client Background
Challenges
More than 30 SKUs through one cell
Packs differ in count, size and stacking behaviour. Any design that requires per-SKU hard tooling turns changeover into the bottleneck, so the cell had to be recipe-driven from the start.
A 5-minute changeover target
Changeover has to be a change of recipe rather than of hardware. Format data lives in the controller, and the operator switches SKUs without tools and without producing trial cartons.
Consistent case forming at 25 cpm
A case that is not formed squarely fails at the sealer, not at the former. Forming therefore has to hold squareness and bottom-seam integrity at production speed, for every one of the thirty-plus formats.
Handling light, compressible packs
Sanitary napkin packs are light and compressible and can be crushed or caused to shift inside the case. The packing robot has to place them without crushing and without letting the stack move before the case is sealed.
How ZRAY Solves It
Project Results
Project Timeline
-
01
Format survey and recipe structure
The full SKU range catalogued; recipe parameters defined so that format differences are handled in the controller rather than in hardware.
-
02
Cell design and build
Case forming, vision packing and sealing modules built as one cell with the recipe library in place.
-
03
Factory run across the format range
Cell run at the ZRAY plant on representative packs across the format range, including changeovers.
-
04
Integration, commissioning and training
Cell installed and commissioned on site; operators trained on recipe-driven changeover for the whole SKU range.
Related Cases
Fixed-Weight Navel Orange Packing Line with In-Line Carton Forming
The industry's first integrated system solution for fixed-weight fruit packing: carton forming, linear multi-head combination weighing and case sealing at…
View CaseBlister Handling and Cartoning Line for Pharmaceutical Tablets
A 70 cartons-per-minute cartoner fed by a 250 ppm blister flow, covering 16 pack formats with a 30-minute changeover.
View CaseBattery Sorting, Honeycomb Tray Forming and Case Packing Line
Three product families and six SKUs: 550 ppm battery infeed through honeycomb tray insertion, telescopic box forming, cartoning and a…
View CaseRelated Videos
Request a Quote for a Similar Project
Send us your carton specs and target output — we reply with a machine configuration and an ROI estimate.